
About us
We are your partner for hygiene, safety, and food safety in the food industry.
Learn more about Brilliant Group
Get to know Brilliant. Discover who we are, what we do, and why we do what we do.

Our History
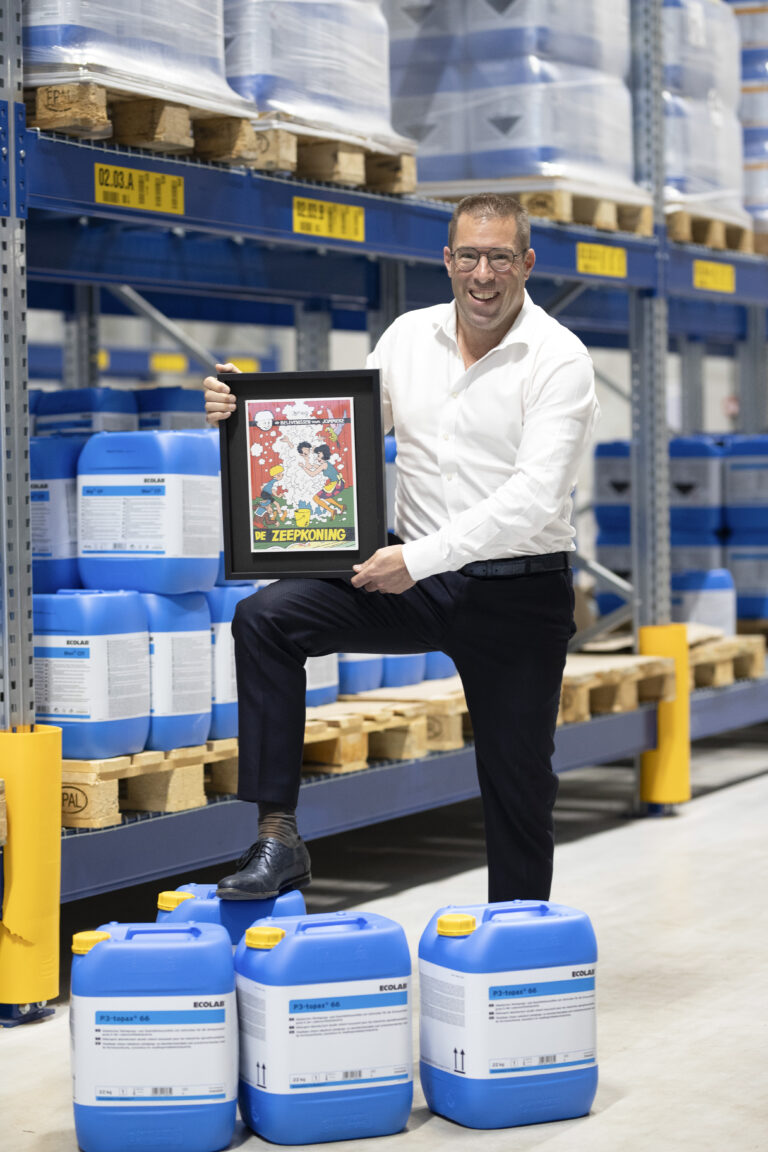
Brilliant Group was born from a well-known player in the cleaning and disinfection market: Ecolab. When Ecolab realized that there were absolutely no parties capable of handling distribution to smaller industrial companies, they came up with a brilliant plan.
That plan involved giving our founder, Marc Rosendahl, the opportunity to establish such a setup himself. This is how Brilliant was born, as a provider of a complete package for hygiene and safety in the food industry.
Brilliant through the years
How we became who we are today. Read our story below.
2003-2005
Starting as Brilliant Food, the certified hygiene partner of Ecolab for the food industry, supplying the FoodGuard Hygiene Management Concept.
2005-2007
Brilliant merged with Hycare Europe, expanding the concept with multiple product groups and evolving into a total solutions provider.
With our specialists, we offer tailored, comprehensive solutions to help companies elevate hygiene and safety standards.
2007-2014
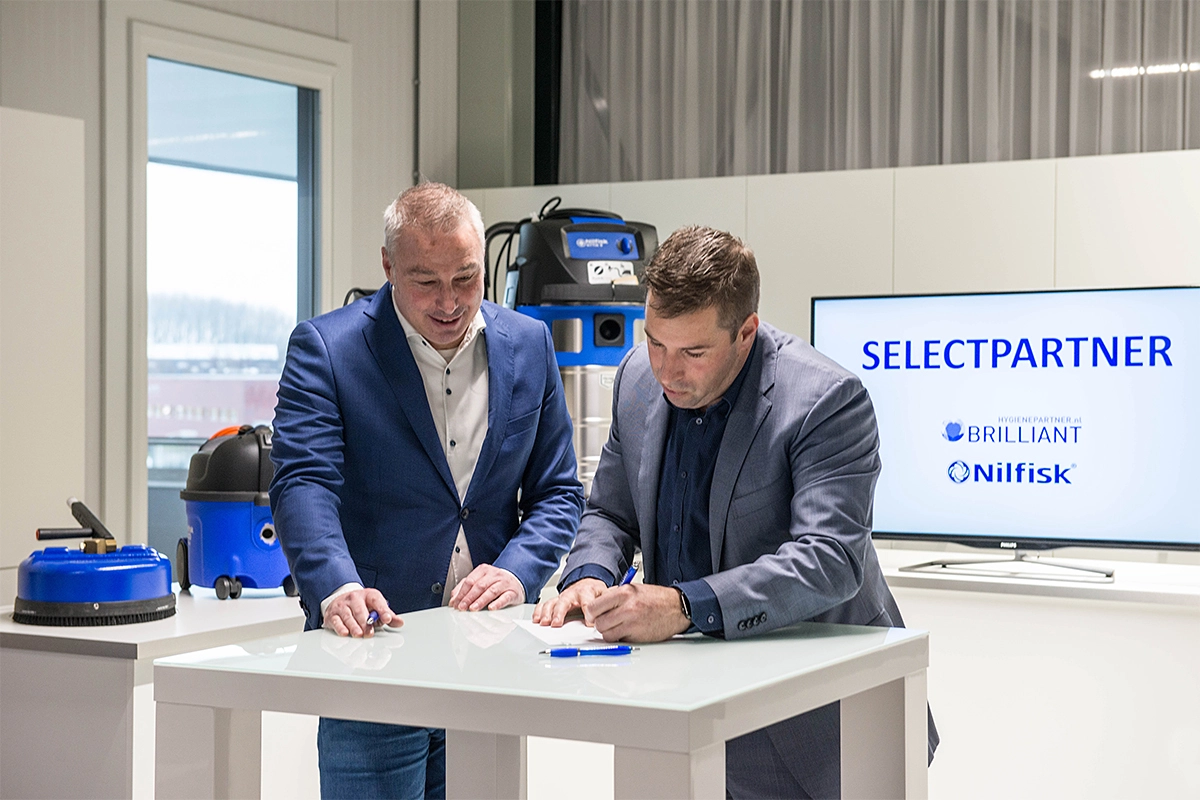
More and more leading suppliers are asking Brilliant to act as the hygiene partner for A-brands.
In addition to Ecolab, we have since become a hygiene partner for PAL International, Vikan, 3M, Honeywell, Nilfisk, Itec, Ansell, Detectamet, EMMA Safety Shoes, Brady, and many more.
2014-2023
Relocation to our first company premises at Typograaf 8 in Duiven. We established new strategic partnerships with partners and suppliers, started importing directly from Asia, and further expanded our range of private A-labels.
Our corporate social responsibility (CSR) policy was introduced, along with electric vehicles and the most fuel-efficient truck. In 2021, we started planning for Typograaf 19...
2023-...
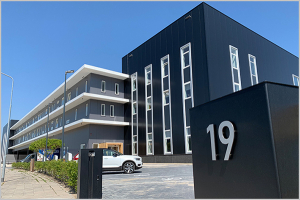
It was time for the next step: our new company premises built to the BREEAM Outstanding standard.
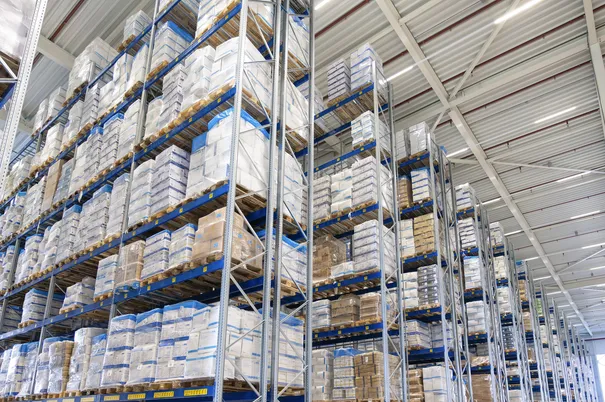
With a larger warehouse featuring 8,000 pallet positions and a team of more than 60 colleagues, we have been advising companies in 14 different food sectors for over 20 years through our own Brilliant Blueprint. We also maintain more than 60 strategic partnerships to guarantee quality, usability, and availability.
Where do we stand now?
A proven approach: The Brilliant Blueprint
We work through a fixed approach, the Brilliant Blueprint, in which we look at the bigger picture: how do employees move through production? Where are the risks? How can processes be made more efficient and safer?
First, we map out the risks based on market knowledge or by conducting an on-site hygiene and (food) safety scan. Then we help with a solution specially tailored for your situation and offer support in its implementation and safeguarding.
Product video
The features of our approach
We are your partner in hygiene, safety, and food safety in the food industry.
Our approach goes beyond just supplying products. Of course, we offer a complete range of hygiene and safety products, from personal protective equipment to cleaning and consumable items, but our added value lies in what we can do for you in addition:
Sustainable initiatives
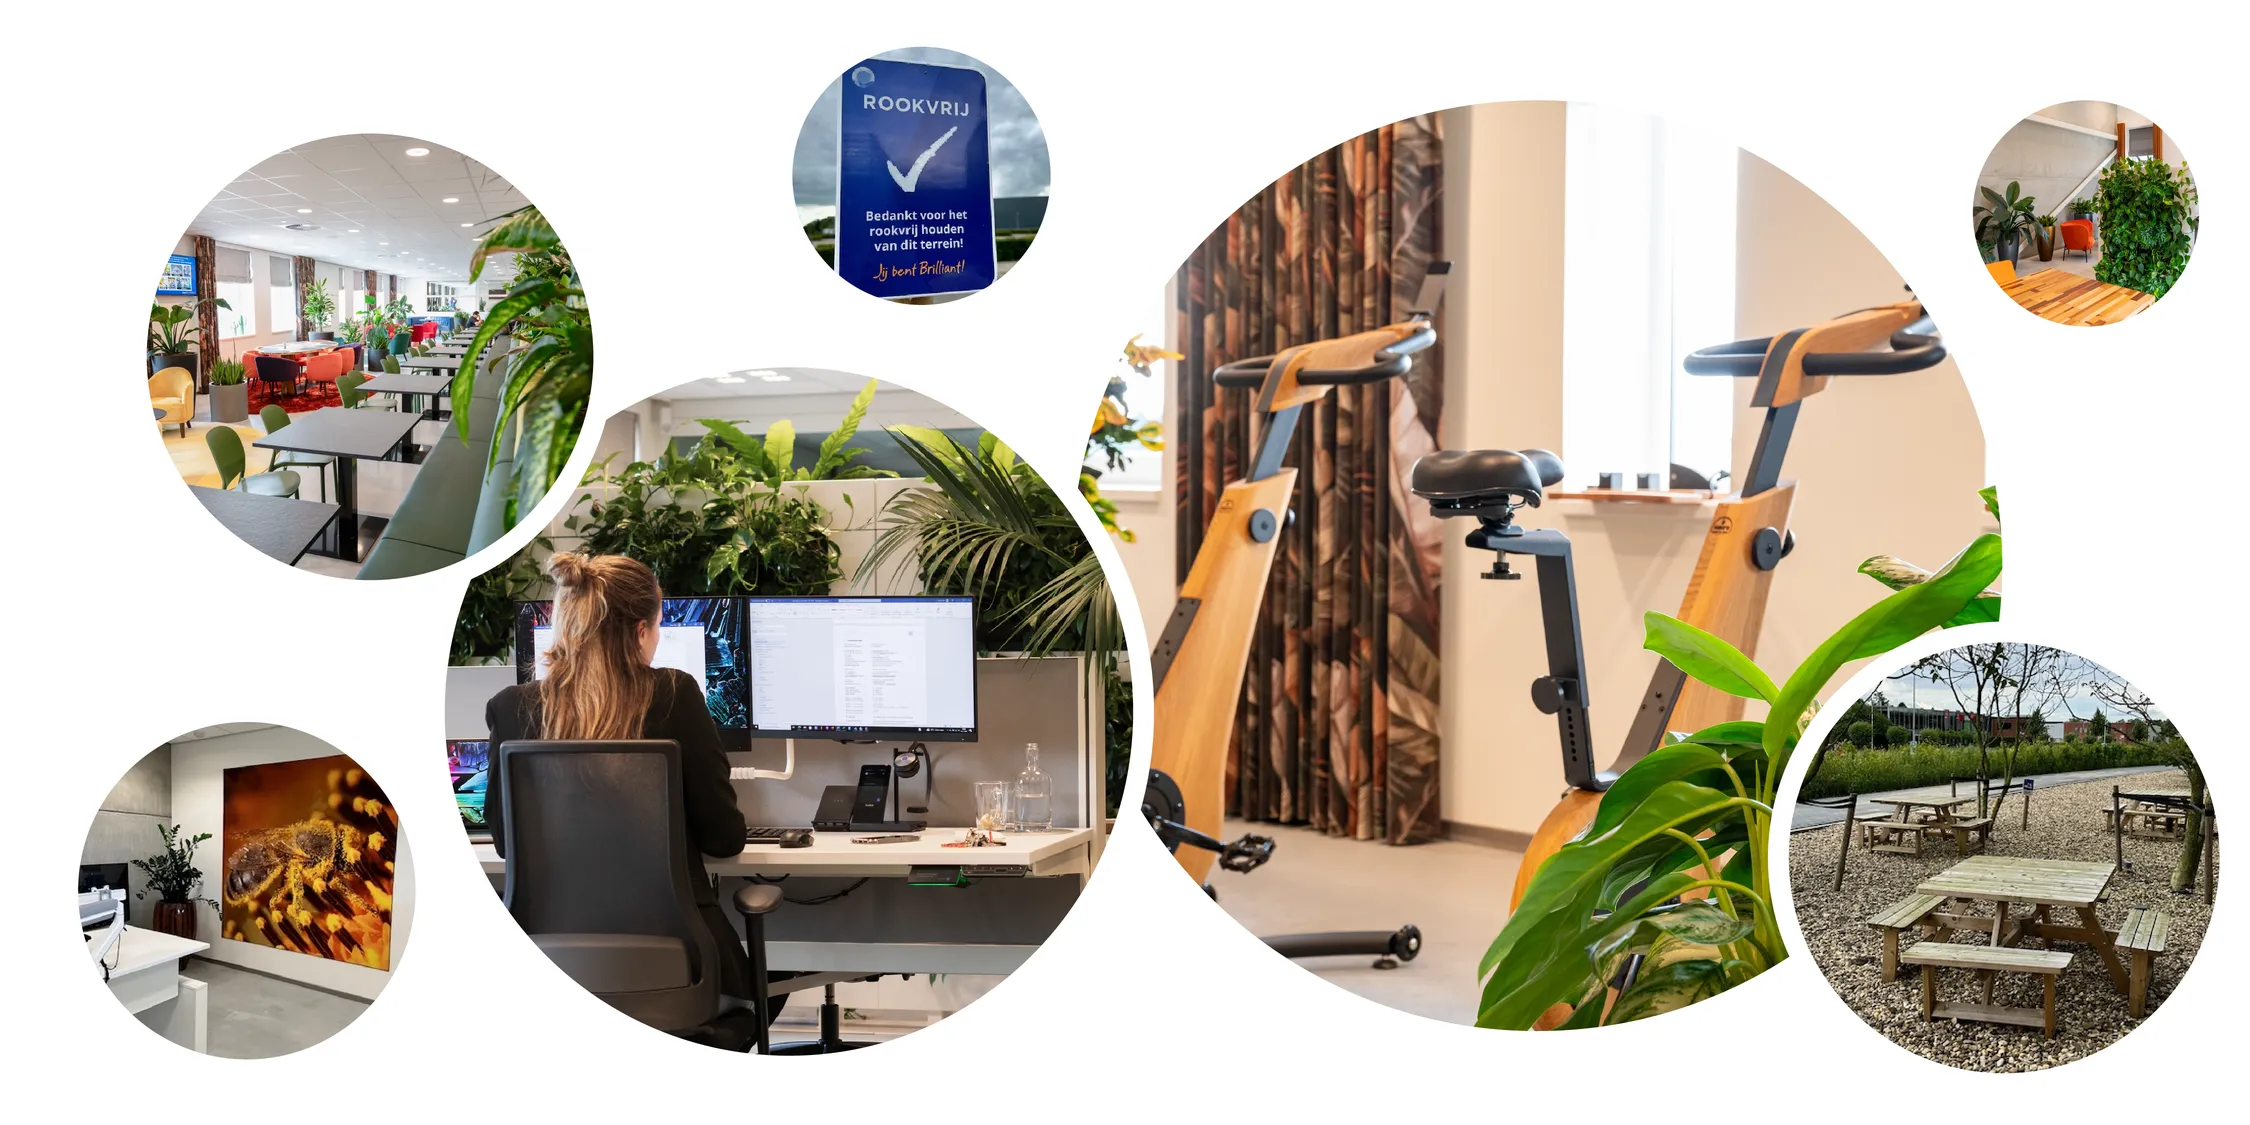
Sustainability is an integral part of our DNA. We believe the future calls for conscious choices in the areas of work environment, logistics, materials, and collaboration.
Our office and warehouse are located together in a building in Duiven. This building is constructed according to the highest sustainability standards and is awarded with a BREEAM Outstanding and a BREEAM In-Use certificate. Additionally, we are certified with WELL Platinum, which demonstrates that the health and well-being of employees are also a central focus.
These certifications emphasize our ambition: to create a work environment that is energy-efficient, future-oriented, and healthy.
Sustainability in our daily operations
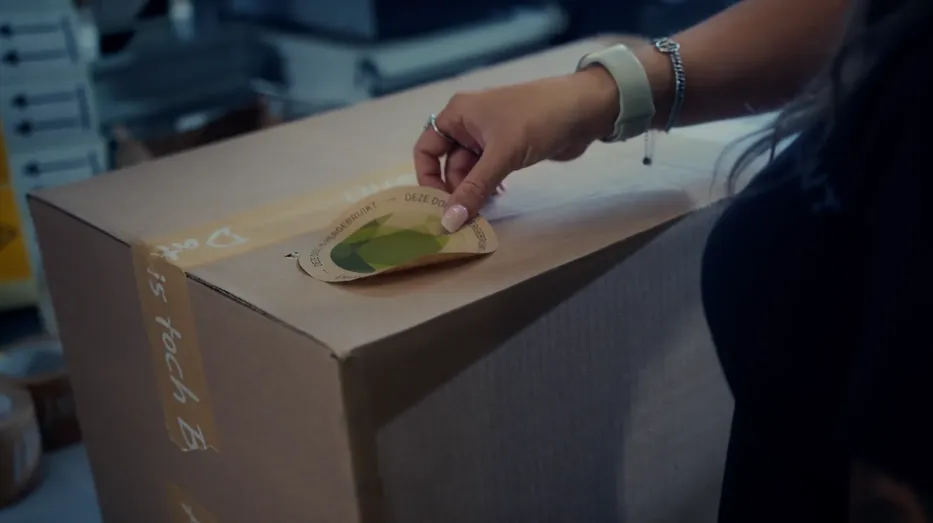
Reuse shipping boxes
In our own warehouse, we use thousands of reused shipping boxes every year, giving packaging materials a second life and preventing unnecessary waste.
Optimizing packaging flows
Critically optimizing packaging flows in our logistics operations so that a large portion of the plastic and cardboard can actually be processed into a high-quality byproduct.
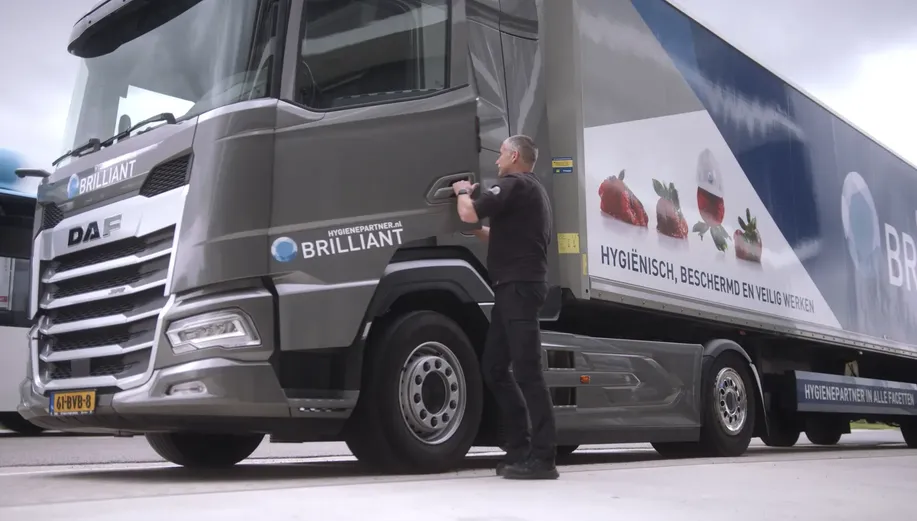
Jerrycan pickup service
We offer a jerry can collection service through which we collect approximately 15,000 used jerry cans from customers each year, ensuring that both the containers and the residual chemicals (approximately 3,000 liters) are processed safely and responsibly through our partner, HSR Group.
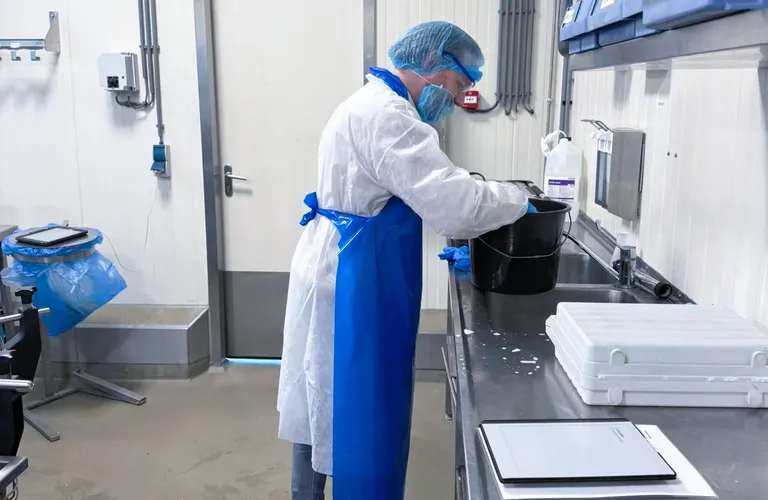
Concentration measurement
A titration service that helps manufacturing facilities optimize the settings for their chemical products, thereby preventing unnecessary overdosing and reducing waste.
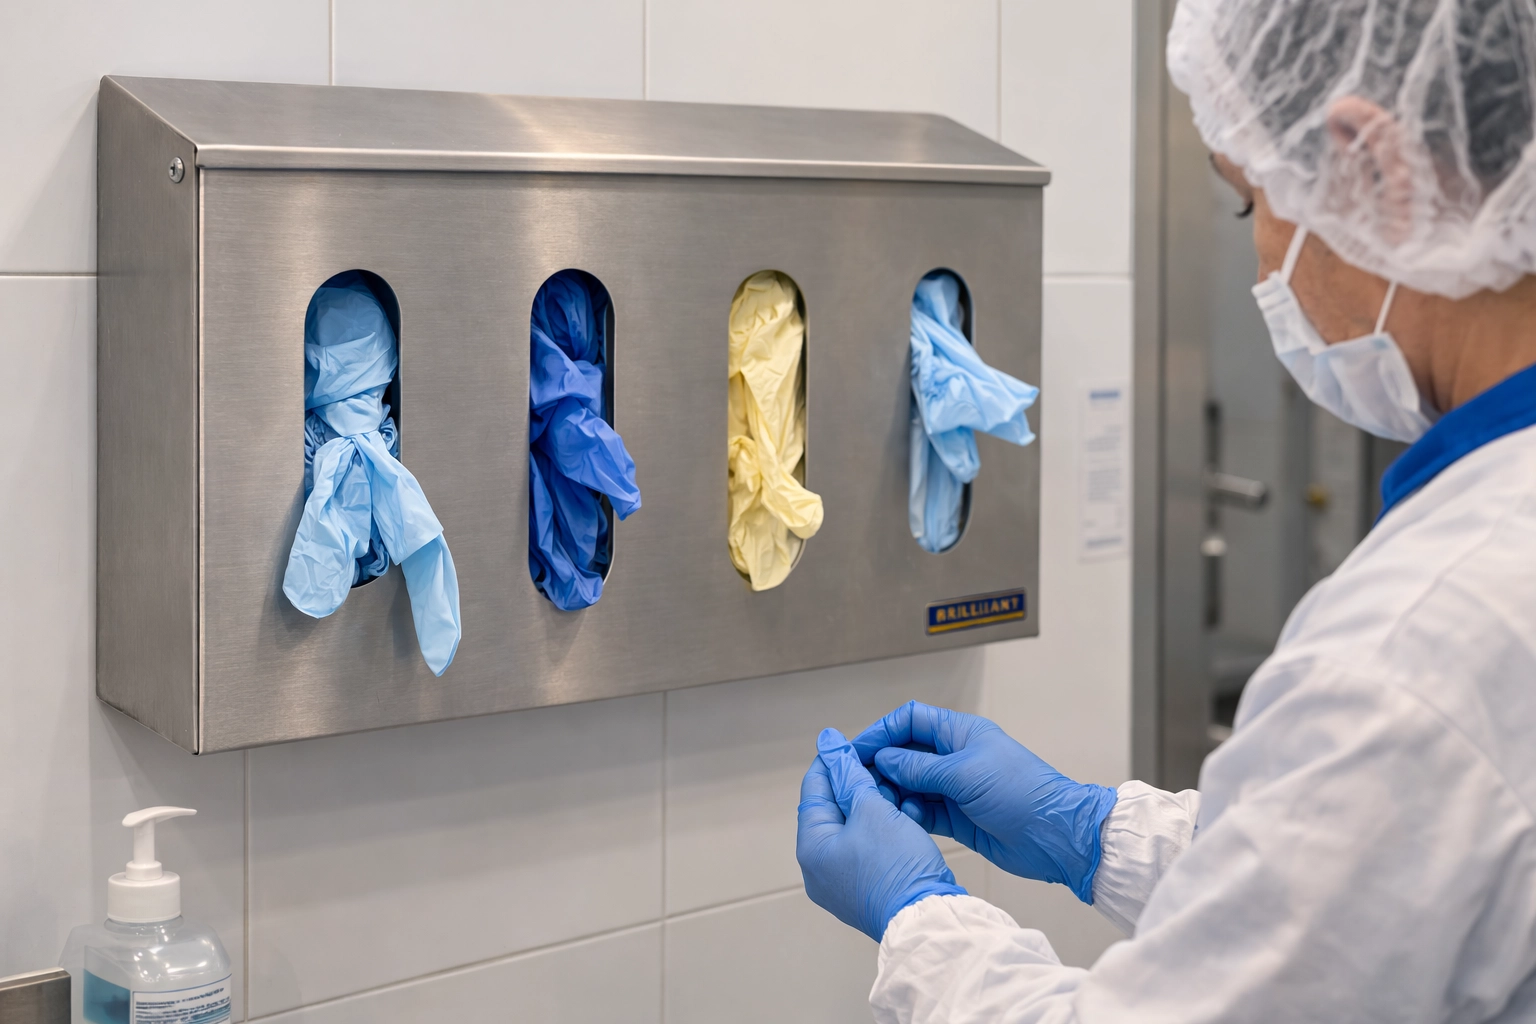
Working together towards a safe and food safe production environment
In the food industry, hygiene and safety are essential to minimise risks. With the right product range and practical advice, you can prevent recalls, production losses, and unsafe situations.
Whether it concerns optimising existing processes or setting up a new production line, we think along with you and provide solutions that can be directly applied on the work floor.